

Returns arriving from your own customers are the most honest quality data you will ever receive, and most buyers bury them in the service department instead of routing them back to sourcing. A simple out-of-box failure log, traced to lot and supplier, closes the loop. This guide builds that loop for detection switches purchases.
Factories measure everything and share almost none of it, not from secrecy but because nobody asks in a form they can answer. Ask for 'quality data' and you get a certificate; ask for the control chart on the dimension that failed last time and you get a conversation.
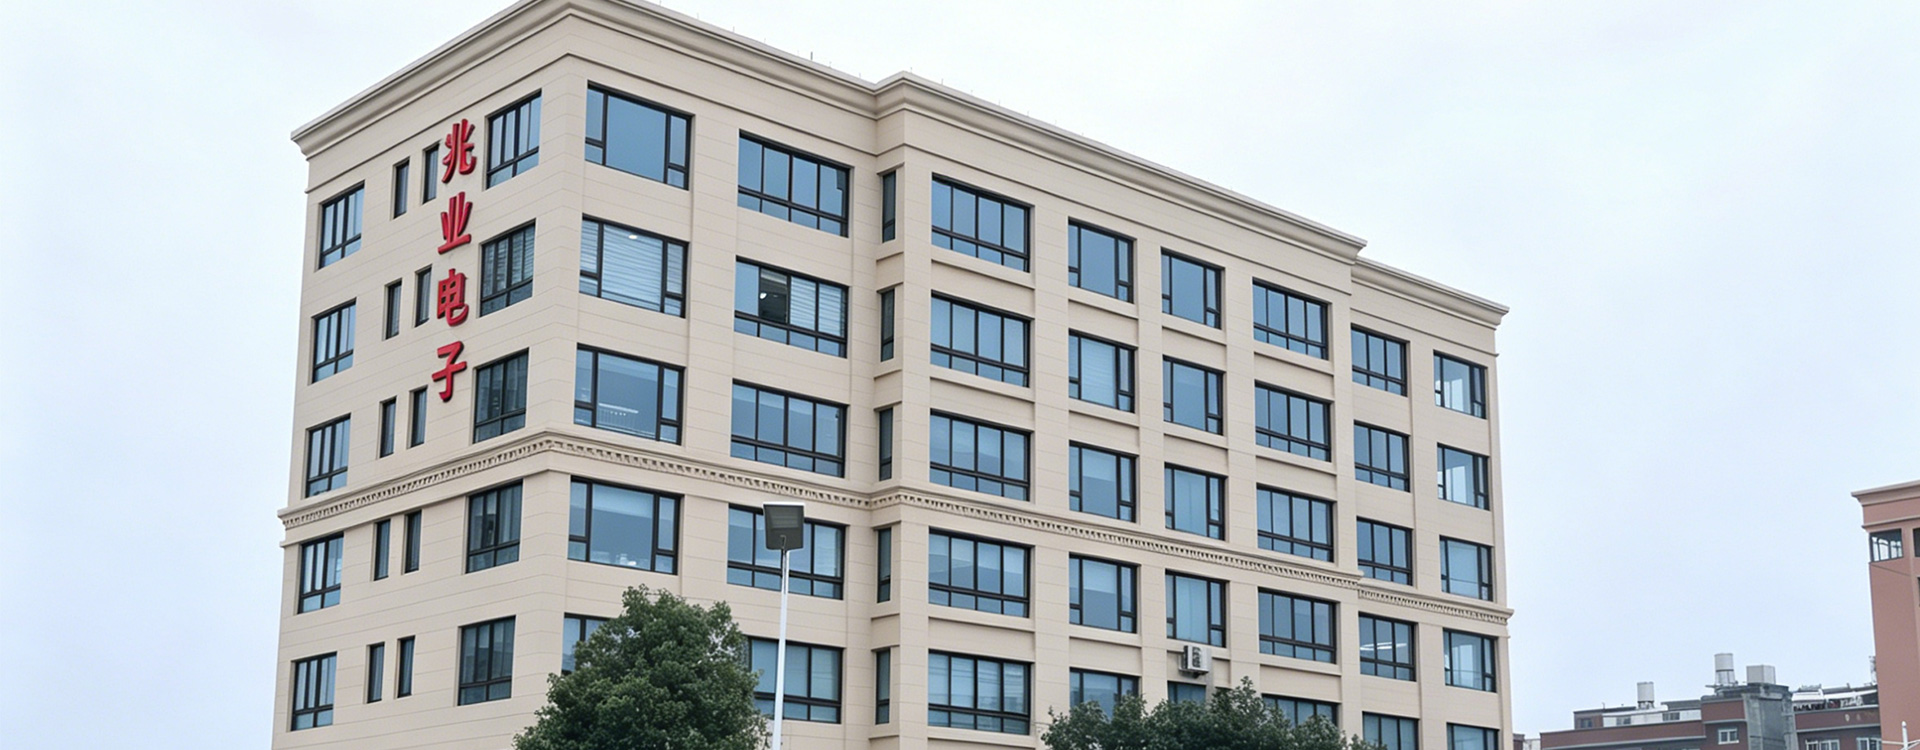
This guide explains how detection switches and micro switches is tested, which standards apply, what certification actually proves, and how buyers can verify quality before, during and after production. It reflects the practices at 温å·å ä¸çµåæéå ¬å¸ (www.zhaoyeswitch.com).
Suppliers make broad quality claims. These are the specific questions that turn a claim into evidence.
Which standard, exactly? Ask for the standard number, not a general assurance.
Who issued the certificate? Recognised third-party bodies carry more weight than self-declarations.
What is the scope? A certificate may cover only part of the product range.
Is it current? Check validity dates and renewal status.
What is the incoming inspection protocol? Ask for the checklist and sampling plan.
What happens when a defect is found? A defined corrective process matters more than a zero-defect promise.
A quality management system (QMS) is the documented set of processes that control how a product is made, inspected and released. Certification such as ISO 9001 confirms that the system exists and is audited; it does not by itself guarantee product quality, but it makes quality repeatable.
Incoming material control: verifying raw materials against specification before use.
In-process control: checking parameters and dimensions during production.
Final inspection: verifying finished goods before packing.
Corrective action: investigating and fixing root causes of defects.
Buyers should treat a QMS as a foundation. On its own it is necessary but not sufficient; it must be paired with genuine product testing.
Different products require different tests, but the categories are consistent across manufacturing:
| Test Category | What It Verifies | Typical Method |
|---|---|---|
| Dimensional | Size and tolerance | Caliper, gauge, CMM |
| Functional | Performance under load | Bench and endurance testing |
| Material | Composition and grade | Spectrometry, certificate review |
| Safety | Compliance with standards | Type testing, Hipot, pressure test |
| Environmental | Resistance to conditions | Humidity, temperature, salt spray |
Ask which of these are performed routinely and which only on request. A factory that tests every batch is fundamentally different from one that tests only the first sample.
Certification confirms that a product or process has been assessed against a standard by an accredited body. It is a valuable signal, but it is not a guarantee of every unit.
Proves: the tested sample complied with the standard at the time of testing.
Does not prove: that every production unit complies, or that the factory maintains the same process over time.
Best practice: combine certification with routine batch testing and periodic re-verification.
For detection switches and micro switches, the relevant certifications typically include UL, CE, RoHS, IEC 61058. Confirm the scope of each certificate covers the exact product you are buying.
A simple incoming inspection protocol is the buyer's last line of defence. It is inexpensive and catches the majority of problems before they reach customers.
Sample the shipment according to a defined plan (for example, per pallet or per batch).
Measure the key specification parameters and record the results.
Functionally test a representative subset.
Verify labelling, packaging and documentation against the approved artwork.
Document results by batch number and raise trends with the supplier.
Reject or negotiate remedies for any lot that fails the criteria.
Keep the data. A buyer who can show three months of measured results has far more leverage in a quality conversation than one who reports only that a batch felt wrong.
Understanding why quality varies helps buyers ask better questions.
Raw material substitution: lower-grade material used to reduce cost.
Tool wear: moulds and dies degrade and produce out-of-tolerance parts over time.
Process drift: settings change without documentation.
Operator variation: manual steps introduce inconsistency.
Sub-supplier quality: components from third parties may not meet the same standard.
A factory that monitors these factors proactively prevents most defects before they occur.
Put quality terms in the contract, not just in conversation. Specify the standard, the sampling plan, the acceptance criteria, the remedy for non-conformance, and the documentation you expect with each shipment.
This protects both sides. The supplier knows exactly what is expected, and you have a defined basis for discussion if something goes wrong.
Recurring quality management means tracking a small set of metrics rather than reacting to individual complaints.
| Metric | What It Measures | Target | Action If Breached |
|---|---|---|---|
| Defect rate | Share of units failing inspection | < 1% | Investigate root cause with supplier |
| On-time delivery | Shipments meeting the agreed date | > 95% | Review capacity and planning |
| First-pass yield | Units passing without rework | > 98% | Analyse process weak points |
| Warranty claim rate | Field failures under warranty | < 2% | Reassess design and testing |
| Documentation accuracy | Correctness of shipping paperwork | 100% | Tighten release checklist |
Track these monthly and review them with the supplier quarterly. A small set of well-understood metrics beats a large set of ignored reports.
The applicable standards depend on your destination market and product category. These are the ones most commonly requested.
IEC 61058: verify the factory can supply the current certificate and that its scope covers your product.
UL 61058: verify the factory can supply the current certificate and that its scope covers your product.
EN 61058: verify the factory can supply the current certificate and that its scope covers your product.
RoHS: verify the factory can supply the current certificate and that its scope covers your product.
UL: request the certificate and confirm validity.
CE: request the certificate and confirm validity.
RoHS: request the certificate and confirm validity.
This is the workflow that turns a quality policy into shipped quality.
Approve the specification and the golden sample in writing.
Verify incoming materials against certificates.
Control in-process parameters and record them.
Run functional and safety tests at defined intervals.
Perform 100% or AQL final inspection before packing.
Complete a pre-shipment inspection with photographic records.
Archive the batch documentation for traceability.
Feed field performance back into design and process improvement.
Statistical process control sounds like a factory-internal affair, but the data is portable: ask for these five outputs each month and you can read the health of your own production without visiting:
| Data Request | What It Shows | Red Flag |
|---|---|---|
| Control chart on the key dimension | Is the process stable or firefighting? | Points hugging one limit â drifted but 'passing' |
| Shift yield trend by line | Where losses concentrate | One chronically low line nobody explains |
| Rework log with reasons | What the process cannot do right first time | 'Cosmetic' used as a catch-all category |
| Capability index (Cpk) on critical specs | Margin between process and limit | Cpk below 1.0 on anything you care about |
| First-pass yield vs final yield | How much inspection is hiding rework | A large, growing gap between the two |
None of this requires the supplier to share anything proprietary â these are aggregates, not secrets. Suppliers already fluent in their own data answer within days; suppliers who cannot produce it are telling you the process is managed by feel, and your {p0l} quality lives in that feeling too.
A certificate confirms compliance with a standard following assessment by an accredited body. A test report records the results of specific tests. Both are useful; the certificate is a higher-level signal, while the report gives detail.
ISO 9001 confirms that a documented quality management system is in place and audited. It makes quality repeatable but does not by itself guarantee a specific product's performance. Combine it with product testing.
Most buyers re-audit annually, or more often if the supplier is new, critical, or has had recent quality issues. Periodic third-party testing complements internal audits.
Document the failure with evidence, notify the supplier formally, and agree a remedy â rework, replacement, credit or return. Track the resolution to confirm the root cause is fixed.
Yes, and it is good practice. Many buyers appoint a third-party inspection company to verify goods before they leave the factory.
It depends on the market: CE for the EU, UL or ETL for North America, and specific standards for food, medical or electrical applications. Confirm the requirement for your destination before ordering.
Check the issuing body's database, confirm the certificate number, scope and validity, and ensure the product in question is covered.
Broadly, yes â but not perfectly. A structured audit and batch testing reveal real quality differences that price alone cannot.
Most sourcing crises are communication cadence failures wearing costumes: nobody agreed who reports what, how often, in which format, so the first real problem arrives as a surprise instead of a trend. The cadence below generalises across the detection switches and micro switches category:
| Rhythm | Content | Why It Prevents Crises |
|---|---|---|
| Weekly during production | One photo line: progress vs plan, any exceptions | Problems surface at day 3, not day 30 |
| Per shipment | Document pack + loading photos before departure | Errors correctable before the goods sail |
| Monthly | Open-order status: dates, quantities, risks | Your planning works on facts, not memory |
| Quarterly | Scorecard review call with named actions | Small grievances get aired before they compound |
| Annually | Strategy conversation: capacity, roadmap, pricing direction | Both sides plan against the same future |
The cadence costs the supplier minutes and buys both sides months of forecast calm. Agree it at kickoff, put it in the order terms, and hold your own side to it as strictly as you hold theirs â cadence failures are rarely one-sided, and the buyer who goes silent between orders has forfeited the right to complain about surprises.
Every quality number in your detection switches supply chain passed through a measuring instrument, and an uncalibrated instrument converts measurement into opinion. The buyer-side discipline is light but non-negotiable:
| Check | What to Ask | What Good Looks Like |
|---|---|---|
| Gauge register | Which instruments touch your critical specs? | A named list, with IDs, per spec |
| Calibration currency | Certificates current for each? | Dates within interval, traceable to standards |
| Calibration body | Who performs it â internal or accredited lab? | Accredited lab for the instruments that gate acceptance |
| Gauge R&R | Do repeatability and reproducibility support the tolerance? | R&R small relative to tolerance on critical dims |
| Record retention | Where do readings live, how long? | Logged per lot, retrievable for the warranty period |
The conversation costs one email and one audit hour, and it separates suppliers who measure from suppliers who glance. A factory with current calibration and gauge studies will argue about real defects; one without will argue about everything â and the second kind of argument never closes.
Ask each detection switches shipment to arrive with â or before â a five-page data pack: page one, the inspection results against the agreed AQL plan with actual counts; page two, the control chart snapshot for the key dimension across the production window; page three, the material certificates for the lots used; page four, photographs of the golden sample comparison; page five, any deviations with the approved concession references. The pack changes the texture of quality conversations permanently: claims become comparisons of two documents instead of memories, and the supplier's own discipline improves because the pack is produced per lot, not per dispute. Buyers who instituted the pack report an unexpected second benefit â the first page alone, trended across lots, is an early-warning system that predicts drift quarters before a customer complaint would.
Buyers track landed cost precisely and working capital loosely, which is odd, because the capital tied up between payment and sale is where importing actually strains. Map the stages once per programme:
| Stage | What Is Tied Up | Typical Duration | Lever |
|---|---|---|---|
| Deposit paid | Cash out, goods not started | 3â6 weeks | Milestone evidence before release |
| Production window | Deposit at risk, no goods to sell | 4â10 weeks | Weekly progress evidence |
| In transit | Balance paid or due; goods unsellable | 3â6 weeks sea, 1â2 air | Insurance, documentation accuracy |
| Customs and delivery | Duty and tax paid ahead of sale | Days to 2 weeks | Correct classification, pre-clearance |
| Receiving to shelf | Goods sellable but not sold | Your operation's number | Demand-linked order sizing |
The map's use is arithmetic honesty: a supplier whose price is 3% lower but whose minimum order ties up two extra months of stock may be the more expensive choice once capital cost is counted. Buyers who present this map internally also defend their order sizes better, because 'we ordered less' stops being timidity and becomes a capital decision with numbers attached.
Incoterms are quoted on every quotation and understood in fragments by most people quoting them. The working summary â the one worth keeping next to the PO:
| Term | Risk Transfers to Buyer | Buyer Should Verify |
|---|---|---|
| EXW | At the factory gate | Is export clearance and trucking actually arranged? Cheapest quote, longest to-do list |
| FOB | On board the vessel at origin port | Which port exactly; who books the vessel; the loading cut-off |
| CFR / CIF | When goods are on board (risk); costs differ | Insurance adequacy under CIF â cover is often minimum by default |
| DAP | At the named destination, before import clearance | Who clears import and pays duty â usually you |
| DDP | After import clearance at destination | Rare from origin suppliers; check the duty assumptions baked into the price |
Two habits prevent most incoterms disputes: name the exact place (not just the term â 'FOB' without a port is a negotiation) and align the term with who actually controls the freight. Buyers with a preferred forwarder buy FOB and control the booking; buyers without one often do better on CIF or DAP from a supplier with competent logistics â the right answer is organisational, not doctrinal.
Products retire, and so do their parts, and programmes that never asked 'what happens at end of life' meet the question as an emergency. The plan costs one page: for each product family, record the expected production horizon as the supplier states it, the last-buy options for parts, the equivalent successor model and its differences, and the stock strategy for the tail â the final years when demand outlives production. Ask the supplier in writing about discontinuation notice periods; twelve months is a reasonable ask, and suppliers answer it more concretely when the question arrives before the last order rather than after. Buyers who plan obsolescence convert retirements into managed transitions â successor qualification run in parallel, tail stock bought at production prices â while buyers who do not meet the same event as a crisis with a premium attached.
Working backwards: goods should be loaded one to two weeks before the holiday, production needs that again depending on scale, and materials need their own lead time â for most programmes this means confirming orders by early December for pre-CNY shipment. The factories that matter most to you are also the busiest then, so capacity is reserved by order date, not by intention.
Shrink the decision loops, not the production: approve samples faster, pre-book inspection slots, pre-clear documents, and release materials deposits on evidence rather than waiting for a weekly meeting. Production itself rarely compresses much; the administrative queue around it often hides two or three reclaimable weeks.
Convert everything to the same landed basis at your warehouse door, using your own forwarder rates for the legs each quote leaves open. The conversion takes minutes with a worksheet and removes the single most common source of false comparisons â the EXW quote that looks cheapest until its missing legs are priced.
Split by risk, not by dogma: consolidate where switching cost is low and volume earns priority, split where a single failure would stop your operation. The practical compromise most programmes land on is a primary with 70â80% and a qualified secondary holding the remainder â enough to keep the secondary warm and the primary honest.
Quotation, specification revision, golden sample record, PO, approvals, inspection reports, shipping documents, and the claim or concession correspondence â the full decision trail. Keep them for the product's service life plus the warranty period plus a year; quality disputes have long memories and short file retention, and only one of those is fixable in advance.
Once a year, review the sourcing programme as a whole rather than order by order: which suppliers earned growth and which coasted; which specifications produced disputes and need rewriting; where the freight calendar was beaten and where it beat you; what the year's claims, concessions and expedites actually cost in total. The output is a one-page reset â supplier actions, specification updates, calendar changes â issued to your own team and your top suppliers alike. Programmes without the post-mortem repeat the year with different dates; programmes with it compound small corrections into visible advantage, and the afternoon it costs is the cheapest consulting the programme will ever receive.
Risk registers have a reputation for theatre â long lists nobody reads â but a five-row register, reviewed quarterly, is a different instrument: it converts background dread into named, owned, dated items. The rows that matter for most detection switches and micro switches programmes:
| Risk | Early Indicator | Mitigation in Place | Review Trigger |
|---|---|---|---|
| Single-source dependency | SKUs without a warm alternative | Qualified secondary, sampled twice yearly | Any supply interruption |
| Quality drift | Rising detection gap between factory QC and third-party findings | Scorecard trend review, PSI tightening | Two consecutive declining scorecards |
| Freight volatility | Spot rates moving against contract rates | Booking calendar, contract rate windows | Quarterly forwarder review |
| Regulatory change | Destination-market standard updates in force dates | Standards watch list per destination market | Annual compliance sweep |
| Supplier concentration in a region | Regional disruption news touching your lanes | Volume split across regions for critical families | Any regional event |
The register's value is the fourth column: pre-agreed triggers convert each risk from a mood into a decision point. Buyers who maintain one spend their worry on schedule, which is cheaper than spending it at two in the morning â and their programmes recover faster, because the mitigation was chosen calmly before it was needed.
Sourcing knowledge is stored dangerously: in one buyer's inbox, one manager's habits, one relationship's goodwill. Staff changes then cost more than the sum of re-reading emails â they cost re-learned lessons and reset relationships. The handover file prevents the reset, and it is genuinely one folder: supplier records with contacts and history, the golden sample register, specifications with revision dates, the scorecard archive, open commitments and promises made, the freight and customs documentation kits, and a one-page 'how decisions get made here' note. Update it quarterly, and the departure of any single person becomes an inconvenience rather than an event. The test of the file is brutal and simple: could a competent newcomer award the next order correctly using only what is written down? Suppliers can tell the difference between a programme with memory and one that starts over every two years, and they price accordingly.
Negotiation outcomes depend heavily on timing, and timing follows a calendar most buyers never draw. The annual rhythm that works:
| Window | Conversation | Why Then |
|---|---|---|
| Quarter end / year end | Volume commitments, annual pricing | Supplier targets are most movable against their calendar, not yours |
| Before the September peak | Freight contracts and booking strategy | Capacity is committed before the crunch reprices it |
| Novemberâearly December | CNY exit plan and pre-holiday orders | Late December asks meet closed factories |
| Spring soft season | Non-urgent volume, spec upgrades | Factory attention and capacity are at their most available |
| After each scorecard review | Corrective actions and relationship asks | Feedback is fresh and goodwill is concrete |
The calendar does not guarantee outcomes; it removes the self-inflicted losses â the price negotiation attempted in the pre-CNY crush, the capacity request raised after the peak was booked. Buyers who negotiate on schedule are also simply calmer negotiators, and calm reads as leverage even when nothing else has changed.
A year into the practices this guide describes, the programme shows signatures no single order can fake: the scorecard conversation runs both directions, because suppliers now bring their own numbers; quotations arrive with assumptions stated and validity dated, because the last three sloppy ones were returned; claims, when they occur, settle on documents within weeks; the second source is genuinely warm and the freight calendar is annotated a year ahead; and the annual post-mortem's one-page reset is already half-executed before the next year starts. None of these required a larger budget â they required the disciplines above, applied past the novelty period. If the signatures are absent at month twelve, the gap is rarely effort; it is usually that one upstream habit â the specification, the milestones, the cadence â was skipped, and the skip is findable in an afternoon.
The disciplines in this guide are not aspirations at 温å·å ä¸çµåæéå ¬å¸ â they are how we operate with long-term customers: specifications written to be checked, milestones tied to evidence, data packs produced per shipment, and a negotiation calendar we plan our own capacity around honestly. We would rather demonstrate the standard on a trial order than describe it in a brochure.
If you are building a new detection switches programme, repairing one that has drifted, or planning volume across the year's capacity windows, send us your specification and your hardest constraint. You will receive a plan you can check line by line â and the measure of its quality is how few of its assumptions you need to remove.
If you want to see how quality is controlled in practice, 温å·å ä¸çµåæéå ¬å¸ (www.zhaoyeswitch.com) is happy to share inspection records, test reports and certification for our detection switches and micro switches. Visit www.zhaoyeswitch.com to learn more and request documentation for your market.
Trang web này sử dụng cookie để đảm bảo bạn có được trải nghiệm tốt nhất trên trang web của chúng tôi.
 English
 Deutsch
 日本語
 한국어


 Điện thoại
Bình luận
(0)