

A supplier's order book is the most honest document they will never send you: it says what they are actually making, for whom, and whether your order will be the one that waits. Backlog depth, product mix and seasonality are readable in a fifteen-minute conversation with the right questions. This guide shows detection switches buyers how to read an order book before committing capacity.
Portfolio design sounds like a corporate exercise and behaves like a practical one: every additional supplier costs management attention, every removed one costs resilience, and the right number is the point where those two costs cross. Most categories never look for that point.
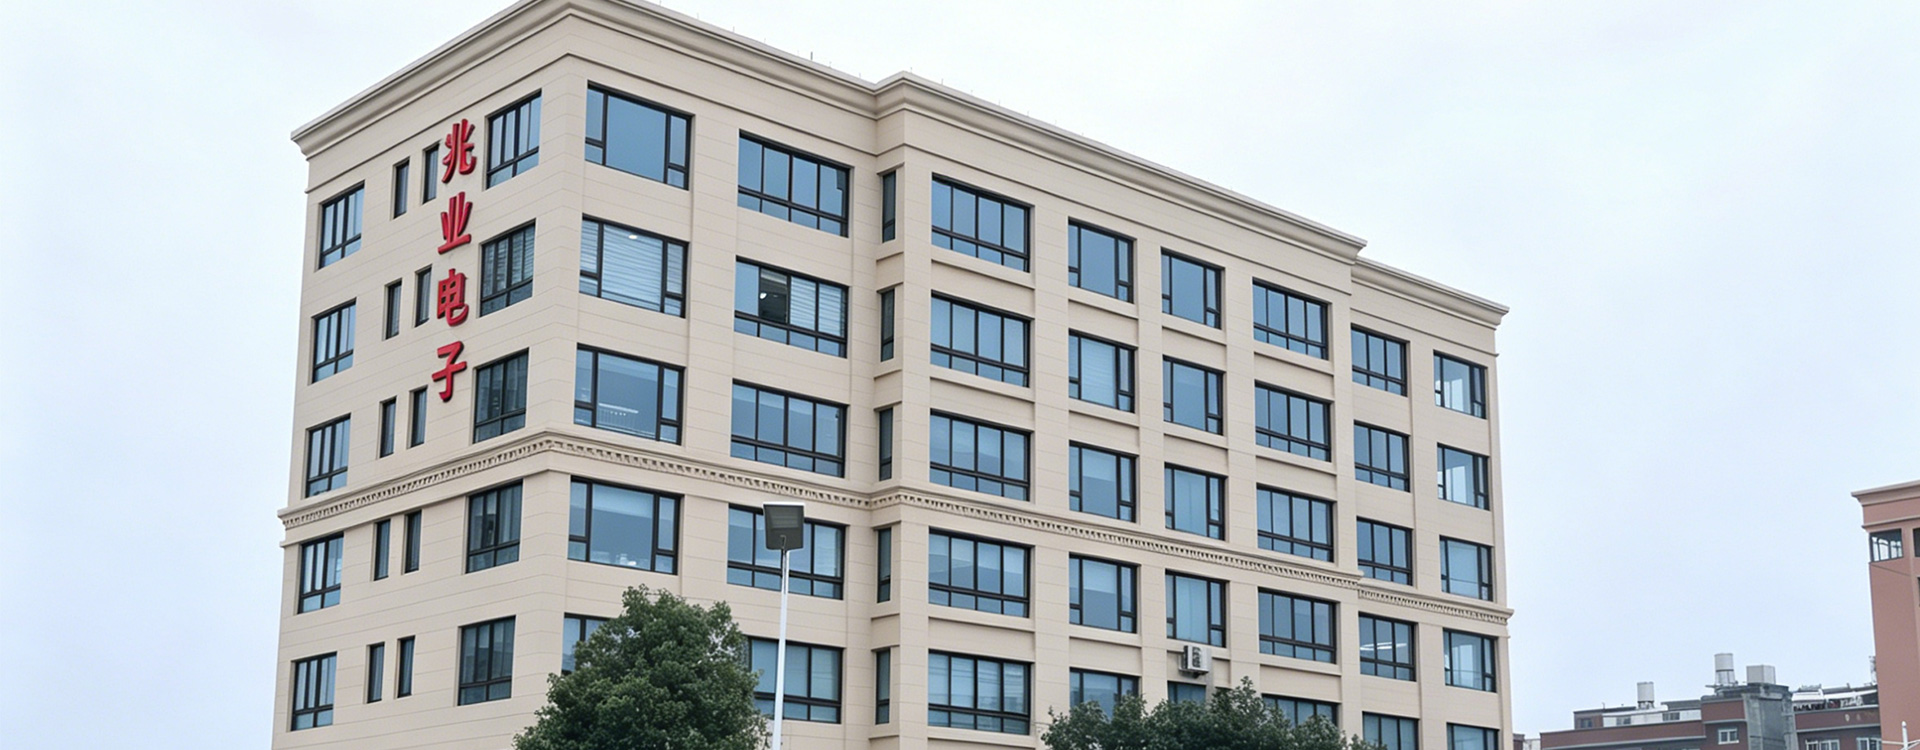
As a manufacturer based in China, 温å·å ä¸çµåæéå ¬å¸ (www.zhaoyeswitch.com) supplies detection switches, tamper-proof switches, micro switches and related products to customers in more than forty markets. In this guide we explain what actually determines quality in this category, how to assess a factory before you commit, and how to build a supply relationship that holds up over years of repeat ordering.
Before you send a request for quotation, be precise about what you are buying. These are the questions that separate a professional sourcing decision from a hopeful one.
What is the production capacity and current lead time? A factory that cannot state monthly capacity in units cannot forecast reliably.
Which quality standards apply, and can they evidence compliance? Ask for IEC 61058, UL 61058 documentation rather than a verbal claim.
Is material traceability documented? Certificates of material origin prevent costly surprises.
What is the defect rate and how are returns handled? Ask for historical data, not a policy statement.
Can they customize to your market's specification? Voltage, sizing, labelling and packaging often differ by country.
What after-sales support is included? Spare parts availability and technical support determine lifetime cost.
What is the total landed cost? Freight, duty and durability matter more than FOB price.
Quality in detection switches and micro switches is the sum of four things: material selection, manufacturing precision, assembly consistency, and testing discipline. A product can look identical to a competitor and behave completely differently after six months in service if any one of these is weaker.
Material grade: the raw material must match the specification, with certificates to prove it.
Manufacturing precision: tolerances must hold across the production run, not just the sample.
Assembly consistency: repeatable processes prevent batch-to-batch variation.
Testing discipline: functional and safety testing must be routine, not exceptional.
For buyers, the practical implication is that you should evaluate capability rather than appearance. A well-equipped factory with documented processes will out-perform a low-cost workshop every time, even if the sample products look the same.
We recommend auditing five dimensions before the first paid order.
Ask for facility size, equipment list, monthly output, and the number of production lines. A factory that can describe its bottleneck process understands its own capacity. Request photos or a live video walkthrough of the production floor.
Confirm certification such as UL, CE and ask to see the internal inspection records. A genuine quality system produces documents: incoming material checks, in-process checks, and final inspection reports.
Understand where raw materials come from and how they are verified. Vertically integrated suppliers control more of the quality chain and are less exposed to sub-supplier problems.
Ask which tests are performed in-house and which are outsourced to third parties. For export markets, third-party test reports from recognised laboratories carry more weight than internal claims.
Evaluate responsiveness during the quotation stage â it is a good predictor of post-sale behaviour. Ask about spare parts availability, technical documentation, and warranty terms in writing.
Most buyers eventually want their own branding, and the best time to discuss it is before the first order. Typical customization includes product sizing, colour, labelling, packaging, and documentation.
Product customization: dimensions, capacity, voltage and configuration tailored to your market.
Branding: logo marking, silk-screen printing, embossing or laser marking.
Packaging: neutral, retail-ready or private-label cartons with your barcode and compliance text.
Documentation: user manuals and compliance statements in your market's language.
Discuss minimum order quantities for customized runs early, because decoration and tooling often set a higher MOQ than the base product.
Unit price is only one part of the equation. The lowest quote frequently carries the highest total cost once durability, freight and returns are included.
| Cost Factor | What to Compare | Hidden Risk |
|---|---|---|
| Unit price | FOB per unit | Ignoring specification differences |
| Durability | Service life | Premature failure and warranty claims |
| Freight | Volumetric weight | Light but bulky shipments cost more |
| Duty and compliance | HS code and certification | Clearance delays |
| Returns | Defect rate | Reputational damage |
| Support | Spare parts and service | Downtime for your customer |
Build a landed-cost model and negotiate on the total. Suppliers respect buyers who understand their cost drivers because it signals a long-term relationship.
The best pricing and priority allocation go to buyers who order predictably. Share a rolling forecast, place consistent orders, and give clear feedback on quality. Factories reward reliable partners with better lead times and preferential treatment when capacity is tight.
It also helps to visit the factory when practical. A single visit reveals more about capability than months of email.
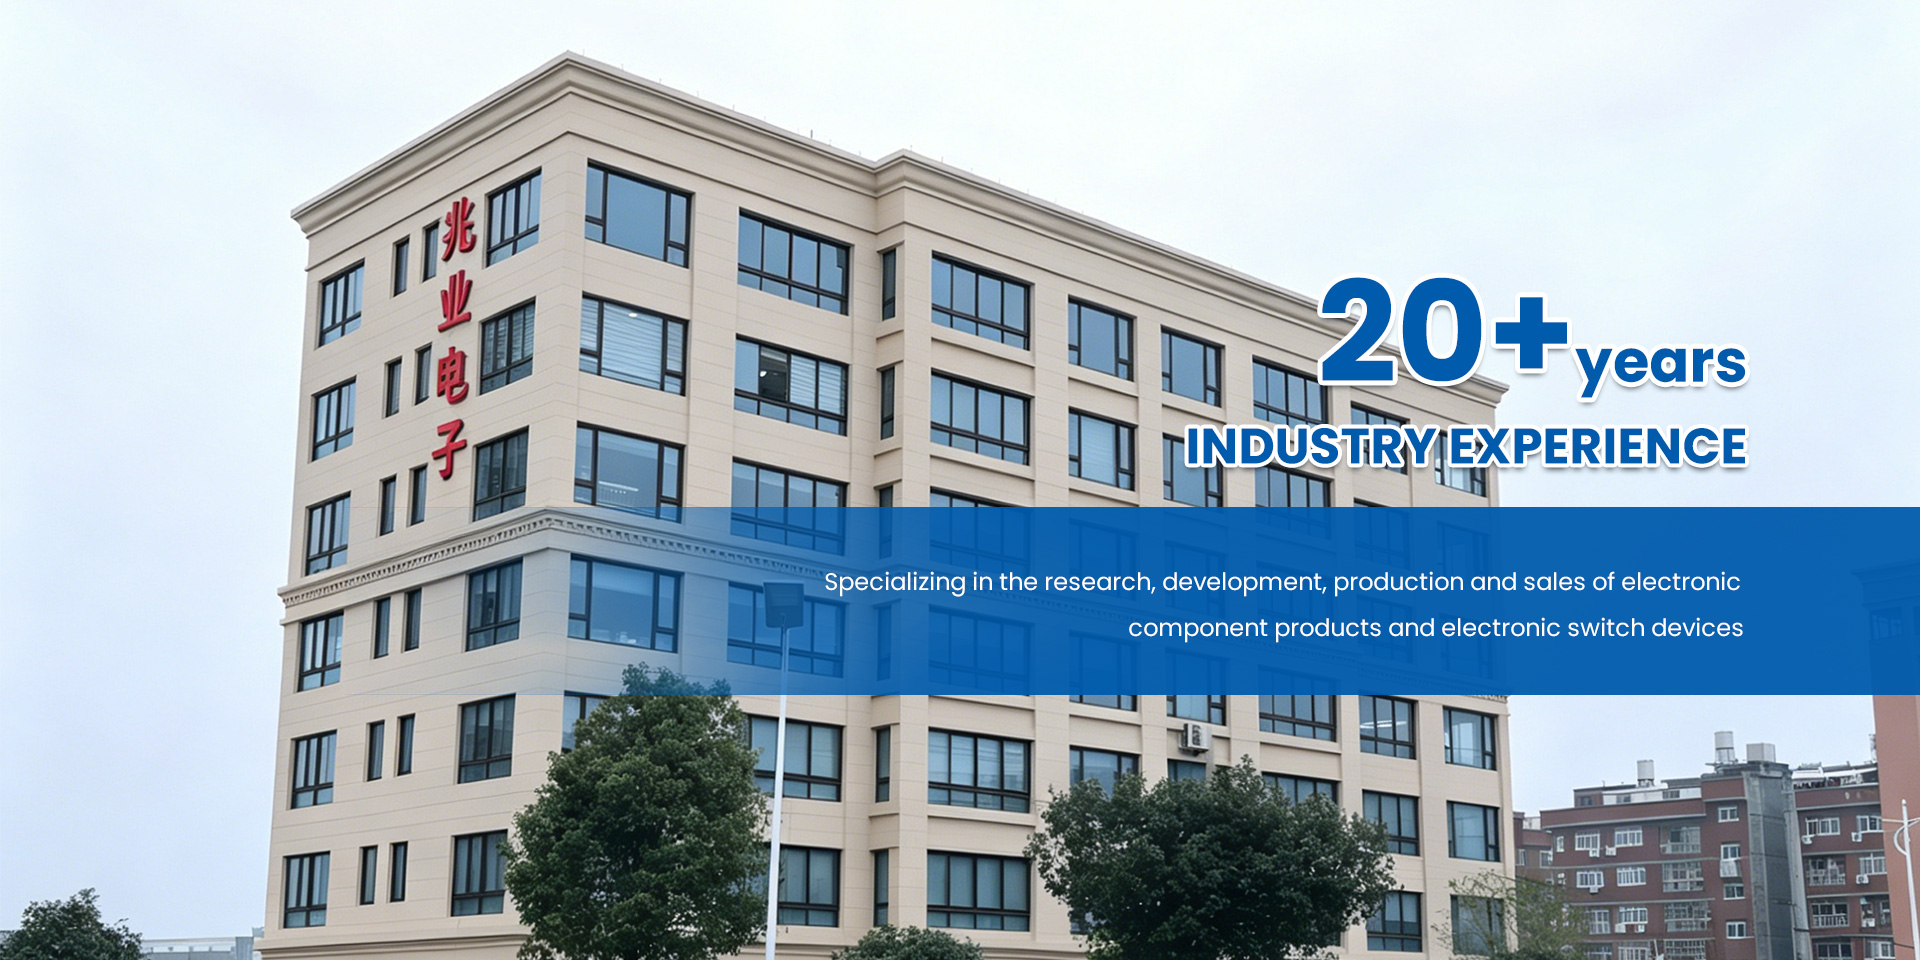
Not every supplier is the same kind of business. Understanding the model helps you choose the one that fits your needs.
| Supplier Type | Control Over Quality | Price Level | Best For | Main Risk |
|---|---|---|---|---|
| Direct factory | Highest | Competitive | Volume buyers | Higher MOQ |
| Trading company | Medium | Higher | Small or mixed orders | Less quality control |
| OEM/ODM partner | High | Competitive | Brand owners | Development time |
| Distributor | Low | Highest | Urgent small orders | Limited customization |
For most buyers building a brand or a stable catalogue, a direct factory with genuine customization capability offers the best balance of quality control, price and flexibility.
Depending on your destination market, several standards and certifications may apply to detection switches and micro switches. Confirming them early prevents costly compliance surprises.
IEC 61058: confirm the factory can supply documentation for this standard where it applies to your market.
UL 61058: confirm the factory can supply documentation for this standard where it applies to your market.
EN 61058: confirm the factory can supply documentation for this standard where it applies to your market.
RoHS: confirm the factory can supply documentation for this standard where it applies to your market.
UL: request the certificate and verify its validity and scope.
CE: request the certificate and verify its validity and scope.
RoHS: request the certificate and verify its validity and scope.
A structured process reduces risk far more than a clever negotiation.
Define your technical specification and target market requirements.
Shortlist three suppliers and request capability data and references.
Order paid samples and test them against your specification.
Audit the chosen factory against the five dimensions above.
Agree pricing, MOQ, packaging and lead times in writing.
Place a trial order and inspect the shipment on arrival.
Review performance with real customers before scaling.
Lock in capacity and lead times for the coming season.
The signals that separate capability from presentation, and how to check each one inside a single visit:
| Signal | What It Suggests | How to Verify It in One Visit |
|---|---|---|
| Order-book composition | Whether your category is core business or filler capacity | Ask what share of output your product family represents, and name their three largest customers |
| Bottleneck disclosure | Whether management understands its own constraint | Ask which process limits throughput and what the current queue is â vague answers mean there is no model |
| Tooling and fixture condition | Maintenance culture, and whether capital spending is being deferred | Walk the tool room: clean fixtures in daily use beat new machines in a showroom |
| Three-year plan | Where capacity, automation and succession are heading | Ask what they are spending on next year, on what, and who signs for it |
| How they answer a bad question | Whether problems get discussed or defended | Ask about the last major customer complaint and listen for sequence: cause, containment, fix |
None of these five signals appears in a certificate, and together they out-predict the certificate: a supplier with a full binder and a silent tool room is a supplier whose quality system lives in the binder, while one with modest paperwork and clean fixtures in daily use is running a system that never needed writing down. The practical discipline is to ask the same five questions on every visit and write the answers down â because the value is not in any single answer but in the comparison, and a page of notes from three suppliers read side by side is more informative than any scorecard built from their own submissions. Capability is not a claim a detection switches buyer has to accept; it is a set of observations anyone can make in ninety minutes with the questions prepared in advance.
MOQ depends on the product and level of customization. Standard configurations typically start lower than private-label runs, which may require tooling or dedicated production. Ask the factory for a clear MOQ schedule by SKU.
A first order typically takes three to six weeks including sampling and approval, while repeat orders are usually shorter. Peak season can extend lead times, so plan ahead.
Order paid samples from at least two production batches, test them against your specification, and require a pre-shipment inspection before release. Documented inspection is more reliable than any sample alone.
Yes. Most manufacturers of detection switches and micro switches offer customization of size, colour, branding and packaging. Discuss the MOQ implications before committing.
At minimum, expect UL, CE, RoHS. The exact requirement depends on your destination market and the application.
Compare landed cost per unit of service life, not FOB price alone. Include freight, duty, defect rate and spare parts in the calculation.
A reliable manufacturer maintains a spare parts inventory and provides technical documentation and support. Confirm the terms in writing before ordering.
Begin with a trial order, measure performance honestly, and share feedback. Consistent ordering earns better pricing and priority.
Delay is the only procurement cost that is never quoted, never invoiced and always paid. A week is the unit that matters, because almost every delay in a supply programme is one week long and almost every one of them was preventable:
Convert the week into money before the meeting: the revenue the missing goods block, the overtime the factory charges to recover, the air freight that replaces a sailing â a number on the table changes what gets escalated and what gets tolerated in silence.
Separate the weeks you own from the weeks you do not: approval, artwork sign-off, deposit release and specification changes are buyer-side weeks; production, inspection and sailing are shared; weather and customs are nobody's. Buyers who count their own weeks usually find two or three they could remove without asking anyone.
Price the cheap insurance: a deposit released on time, a pre-booked inspection slot, a second document check â each costs minutes and each removes a class of week, which is why they are the first things to be cut and the last things that should be.
Track weeks, not milestones: milestones are reported as met or missed; weeks accumulate and show whether a programme is drifting before any milestone is technically late â the earliest honest signal available.
Put a date on every open item: an item without a date is an item that will consume someone's week later, and usually the week before shipping, which is the most expensive week in the calendar.
The discipline pays twice: once in the weeks recovered, and once in the arguments avoided, because most escalations in a supply relationship are not about the delay itself but about who was supposed to know. A buyer who tracks weeks, prices them and states them early converts a recurring confrontation into a shared schedule â and suppliers, who live inside their own capacity calendars, respond to a buyer who understands what a week costs them far better than to one who simply repeats the ship date. The number is not a threat; it is the reason the schedule is worth protecting.
The count follows from three variables, and from nothing else:
Concentration risk: what a single failure would cost in revenue, customer commitments and recovery time â a category that stops a line needs a second source regardless of its spend, while a cosmetic category can live with one.
Volume viability: the smallest order that keeps a supplier interested enough to protect your slot â splitting volume below that line buys a second name and loses both suppliers' attention.
Management bandwidth: every supplier consumes reviews, visits, reconciliation and relationship work â the portfolio that ignores this number is designed for a procurement team that does not exist.
Then choose the shape deliberately: single source with a contingency, dual source with a split ratio, or a primary plus a qualified standby that receives token volume to stay qualified â three shapes, three different maintenance costs.
Write the trigger for changing the shape: the volume, risk or performance event that would justify adding or removing a source â without a written trigger, the portfolio changes only after a failure, which is the most expensive moment to redesign it.
The map's value is that it replaces a number with a reason: the category with two suppliers because a disruption once happened and the category with two because the arithmetic says so look identical on a spreadsheet and behave completely differently in a review, because only one of them can explain itself. Buyers should also expect the map to be uncomfortable in places â a critical category carried by one supplier because splitting it seemed administratively heavy is a finding, not a preference, and the map is what makes that visible before the failure rather than during it. One page per category, reviewed annually, is enough.
A qualification photographs the present; the roadmap conversation asks about the direction of travel:
| Question | What a Strong Answer Sounds Like | What a Weak Answer Reveals |
|---|---|---|
| What are you investing in next year, and what will it change? | Named equipment or systems, a budget, a date and the constraint it removes | 'We are always improving' â improvement without a constraint is a slogan |
| Which part of your process is closest to its limit? | A specific bottleneck, its current utilisation and the plan for it | No acknowledged limit â which means the limit will be discovered by a customer |
| What happens to this factory when the current owner leaves? | A named successor, a transition plan, and what the family or group intends | Discomfort and a change of subject â the succession risk is real and unpriced |
Three questions, one meeting, and a page of notes that changes how the relationship is managed: a supplier investing in the constraint that limits your orders is a supplier whose capacity will grow with you, while one that cannot name its bottleneck will meet your next volume increase with an apology. The succession question is the one buyers skip and the one that most often decides a supply relationship's fate â a factory under new ownership re-prices, re-prioritises and sometimes re-tooled for a different customer entirely, and the buyer who knew the plan two years earlier had time to prepare a second source instead of improvising one. None of this appears in detection switches audits, and all of it appears in outcomes.
The first order is always the most expensive unit a buyer will ever purchase, and the reason is structural rather than commercial:
Setup is a fixed cost spread over a variable quantity: tooling, fixtures, programming, artwork, first-article inspection â the same money divided by a hundred pieces or ten thousand, which is why a sample quotation and a volume quotation rarely resemble each other.
The learning curve is real and it is yours to pay for: the first thousand units carry the operator's hesitation, the process engineer's experiments and the yield that improves only with repetition â suppliers price this in, whether or not they itemise it.
Small orders buy attention rather than efficiency: a factory scheduling a small run around larger ones pays for the disruption, and that cost is legitimate â the question is whether the buyer needs the attention or the volume.
Repeat orders are where the saving lives: the fourth order of the same specification costs less to make, less to inspect and less to administrate than the first â buyers who change specification every cycle restart the curve and pay for the restart every time.
Consolidate before you negotiate: combining variants, lengthening the run or accepting a standard colour often removes more cost than a percentage point negotiated off the unit price.
The practical implication is that early negotiations should be about structure rather than price: how much of the setup is charged, whether it amortises across an agreed volume, what the price looks like at three quantity bands, and what would have to be true for the second order to cost less. Suppliers answer these questions readily because the arithmetic is theirs, and buyers who ask them discover that the price they were negotiating was largely a reflection of quantity, timing and variety â three variables they control. The first batch is expensive; treating every batch as a first batch is a choice.
Requests to co-invest arrive dressed as partnership and are, in substance, a financing decision with a supply contract attached:
Establish what the money buys and who owns it: a specific machine, a mould, a line extension or general capacity â with ownership, serial numbers, location and a register both sides sign, because funded assets that cannot be identified cannot be recovered.
Ask what happens if the relationship ends: buy-back rights, removal rights, transfer to another supplier, or amortisation against future orders â the exit terms are the whole difference between an investment and a gift.
Price the alternative: what the same capacity would cost from a different supplier, and what staying without it would cost in lead time and lost orders â co-investment is only rational when it beats both.
Tie disbursement to milestones: installation, commissioning, first-article approval, volume ramp â money released against evidence rather than against enthusiasm.
Secure the capacity explicitly: if you funded the machine, the reservation mechanics should say so in writing â an investment without allocation priority is a donation to somebody else's largest customer.
Co-investment is neither good nor bad in itself: in concentrated supply bases with long qualification cycles it is often the only way capacity gets built for a buyer's product at all, and suppliers fund capacity for the customers who fund it first. What separates a sound arrangement from a costly one is documentation â ownership, exit, milestones and allocation, four clauses that take an afternoon and decide the outcome years later. Buyers who decline should decline explicitly and early, with the reason stated, because a vague no is read as a maybe and the capacity gets committed elsewhere while the buyer believes the conversation is still open.
Suppliers perform in audits and in crises; the question is what they are like on an ordinary day:
How fast does a routine question get answered? the quotation clarification, the shipping document, the small change request â response speed on trivia predicts response speed when the subject is expensive.
Does the paperwork arrive correct the first time? an invoice, a certificate, a packing list â repeated small errors are a system finding, not a clerical one, and they multiply at volume.
Is the account manager still the same person? stability of contact is the cheapest indicator of a stable organisation, and constant rotation is a symptom worth investigating rather than tolerating.
What does the factory look like when no one announced a visit? the unannounced walk-through â housekeeping, WIP order, people at stations â is the only observation the supplier did not stage.
Are commitments dated, or adjectives? 'soon', 'as discussed' and 'shortly' in ordinary correspondence become real delays in extraordinary weeks â the language of routine emails is the language of a crisis.
The test's logic is that ordinary days are most of the relationship: a supplier who is reliable on a Tuesday will usually be reliable in a crisis, because reliability is a habit rather than a performance, while one who is charming in meetings and slow on emails is telling you exactly how the next dispute will go. Buyers should score the ordinary day deliberately â response time, first-time-right documentation, contact stability â and review it quarterly alongside price and quality, because these are the numbers that predict the year, and they are available long before any audit would reveal them.
It follows from three numbers rather than a rule: the cost of a single failure (concentration risk), the smallest order that keeps a supplier interested (volume viability), and the reviews and visits your team can actually sustain (management bandwidth). Then choose a shape deliberately â single source with a contingency plan, dual source with a split ratio, or a primary plus a qualified standby on token volume â and write the trigger that would justify changing it. Most categories need fewer suppliers than they have, and more contingency than they planned.
Change control is the contractual requirement that a supplier notify you before altering materials, processes, tooling, sub-suppliers, software or labelling â with a notice period, test evidence and an approval route. It matters because most quality failures that reach customers are built by a changed process rather than a bad one, and the change was usually made to protect a delivery date. Certificates describe the system a factory had; change control determines whether the product you receive next quarter is the product you qualified.
Because quality drifts rather than collapses: tolerances ease, inspectors rotate, sub-suppliers change, and the attention that the account received while it was new migrates to the next new account. Drift is invisible in shipment-level inspection and visible in trends â so measure what moves (dimensional variation, complaint categories, deviation counts), re-audit on a cycle rather than on suspicion, and keep sampling the documents nobody asks for. Year two is where a relationship is either institutionalised or quietly lost.
Shipping marks exactly as they will appear on the cartons, handling symbols, the description matching the commercial invoice word for word, gross and net weights, dimensions and volume, batch or lot numbers, and the document set reference. The purpose is reconciliation: any field that cannot be checked against the goods, the invoice or the transport document adds no control. Prepare it before the container is stuffed, and have someone with authority to stop the loading sign it.
Map the stages once with real dates from three past orders, then attack the three usual culprits: approval loops with no owner or deadline, material procurement waiting for a deposit that could have been released against a signed order, and queue position assumed rather than booked. Most buyers find two stages running in sequence that could run in parallel, and a ship date that was optimistic because nobody had asked the factory for a slot calendar. The cycle is usually shorter than the organisation believes â the difference is planning, not pressure.
If you are sourcing detection switches and micro switches for distribution, OEM production or a project, 温å·å ä¸çµåæéå ¬å¸ (www.zhaoyeswitch.com) would be glad to share our experience and provide samples. Visit www.zhaoyeswitch.com to explore the catalogue, request a quotation, and discuss customization for your market.
Trang web này sử dụng cookie để đảm bảo bạn có được trải nghiệm tốt nhất trên trang web của chúng tôi.
 English
 Deutsch
 日本語
 한국어



 Điện thoại
Bình luận
(0)